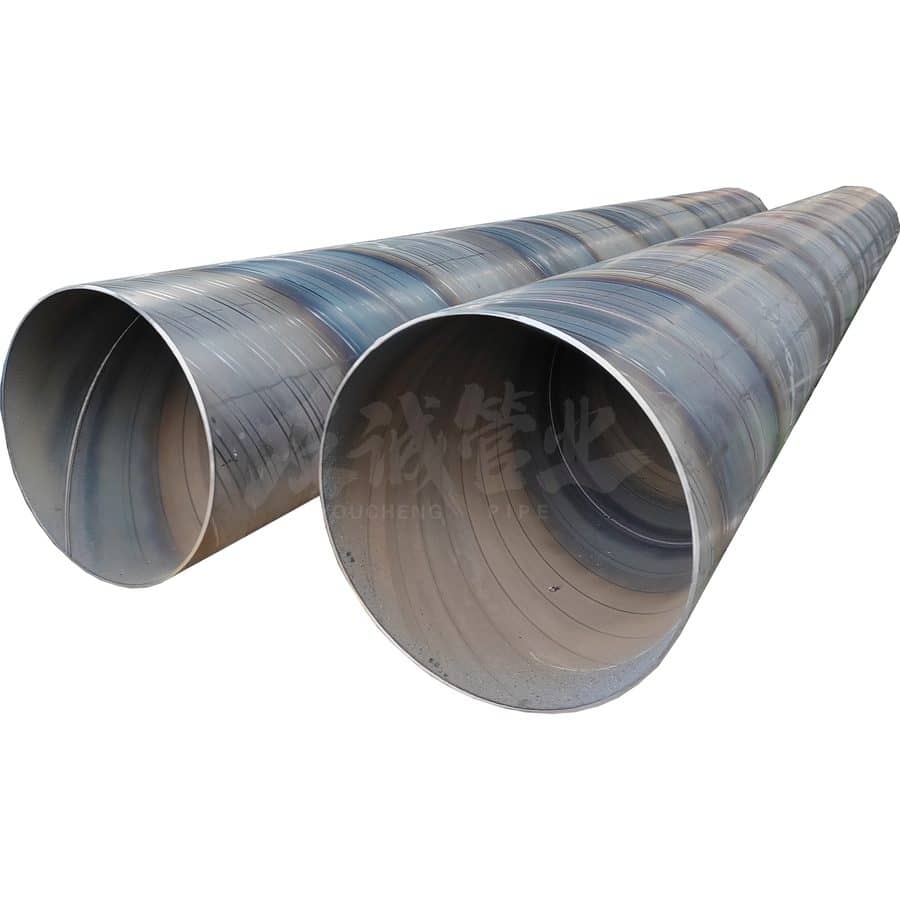
Spiral submerged arc welded pipe from DN200 to DN3800, made strip-by-strip in our own plant.
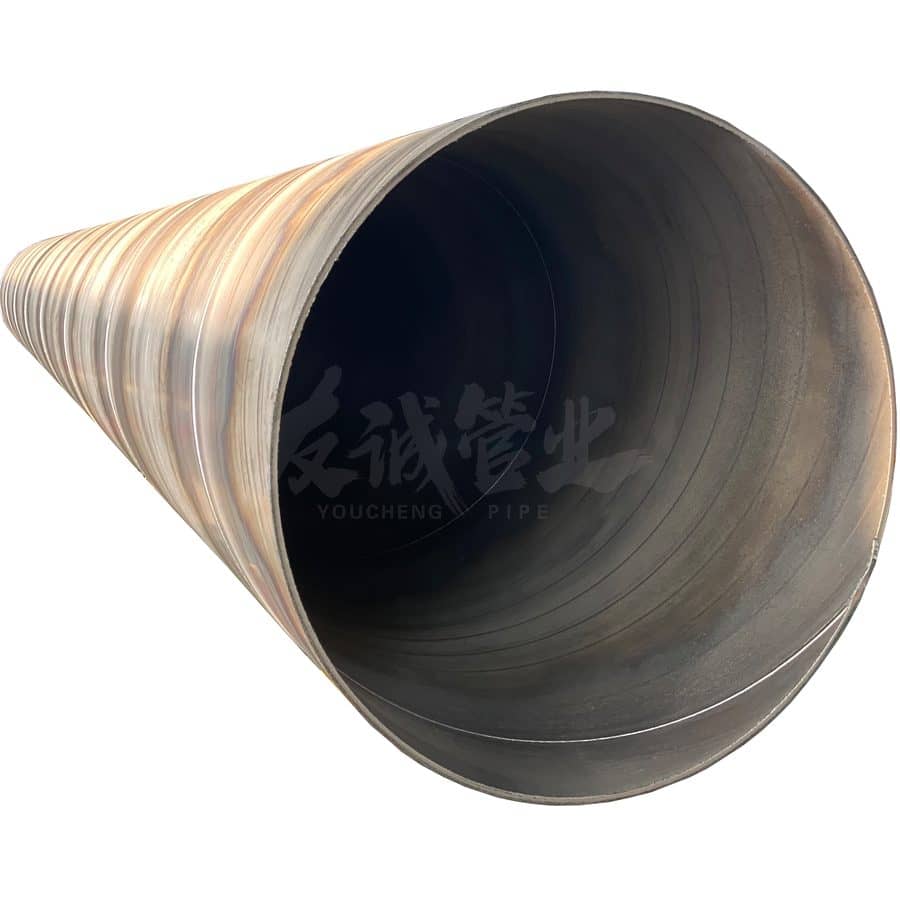
Spiral submerged arc welded (SSAW) pipe is made by helically bending a hot-rolled steel strip and welding the seam from both the inside and outside. Because the strip width sets the diameter, a single line can economically produce very large diameters — which is why SSAW is the standard choice for water transmission, piling, structural columns and low-to-medium pressure service.
At Youcheng we run the whole process in one plant: coil inspection, levelling and edge milling, three-roll forming, inside-then-outside submerged arc welding, ultrasonic testing, cut-to-length, hydrostatic testing and marking. Keeping it under one roof means the heat number of the coil follows the pipe all the way to the bundle tag.
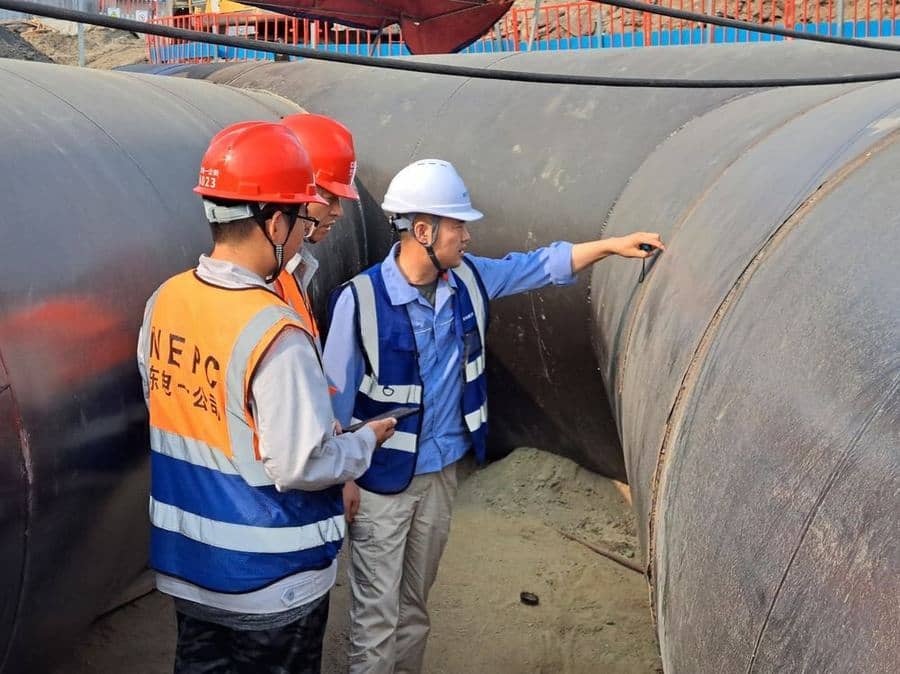
Weld integrity is the part buyers care about most. Every metre of the seam is ultrasonically tested, X-ray spot checks are taken on the pipe body and in the weld start/stop zone, and any indication is repaired by qualified welders and re-tested before the pipe can move to hydro-testing. Test pressure, holding time and result are recorded against each pipe.
Tell us the medium, design pressure, laying method and standard you need. We will come back with a wall-thickness check, coating recommendation, packing proposal and a firm quotation — usually within 24 hours.


| Outside Diameter | 219 – 3820 mm (DN200 – DN3800) |
| Wall Thickness | 5 – 25 mm |
| Length | 6 – 14 m, or cut to order |
| Steel Grade | Q235B / Q355B / L245–L450 (Gr.B–X65) |
| Standard | GB/T 3091, GB/T 9711, SY/T 5037, API 5L, EN 10219, ASTM A252 |
| Weld Type | Double-side submerged arc spiral weld |
| NDT | 100% UT of weld seam + X-ray spot check |
| Hydrostatic Test | Per standard, 100% tested, records kept |
| Pipe End | Plain / 30° bevel / with end protector |
| Surface | Bare black, or varnish / oiled on request |
| Certificate | Mill test certificate EN 10204 3.1, ISO 9001 |
Every pipe passes through the same controlled route, with inspection points at each stage.
Every coil is checked for mill certificate, chemical composition and mechanical properties before it enters the line.
The strip is uncoiled, levelled and its edges milled to guarantee a stable, full-penetration weld groove.
The strip is bent on a three-roll forming bed into a helix at a controlled forming angle and gap.
Submerged arc welding is applied first inside then outside, at least two passes inside and outside for heavy wall.
100% ultrasonic testing of the weld seam plus X-ray spot inspection; defects are repaired and re-tested.
Pipes are cut to ordered length, end-prepared, then hydrostatically tested at the specified pressure with records kept.
Dimensional check, visual check, then stencilled marking and bundling according to the packing list.
FBE / 2FBE / 3PE / TPEP systems for buried gas, water and sewage lines.
Direct-buried polyurethane pre-insulated pipe for district heating networks.
Steel-jacket steam insulation for high-temperature steam transmission.
Plastic-coated pipes for water supply, fire fighting, mining and cable protection.
